





What Is The Die Casting Process for Components? A Complete OEM Buyer’s Guide
Are you a purchasing manager, technical director, or operations lead struggling with inconsistent supplier quality, hidden tooling costs, or European/US compliance headaches? This guide breaks down what is the die casting process, its cost drivers, and how a Chinese OEM partner can deliver precision parts at 30–50% lower total cost.
⚡ Response within 24 hours • NDA available • ISO 9001:2015 certified
⚠️ The 6 Hidden Costs of Sourcing Die Cast Components the Wrong Way
In our 20 years of exporting OEM components to 30+ countries, we see the same six mistakes repeat. Let’s be honest with you:
1. Inflated Western Pricing
US/EU die casters charge $4–8 per kg for aluminum parts. The same OEM-grade component from our Chinese supply chain: $1.80–2.80 per kg — a 45–60% cost saving before shipping.
2. Inconsistent Quality
Non-specialist suppliers deliver porosity rates above 5%, leading to rejection slabs of 15–25% at incoming inspection. Your line stops. 25% rejection = delayed time-to-market.
3. Shipping Cost Overruns
Poorly packed die cast components from Asia arrive with 3–7% transit damage rates. Re-shipping a 20ft container from China adds $4,800–6,200 to your landed cost.
4. Lead Time Delays
Typical EU die casting lead time: 10–14 weeks. Our clients average 4–6 weeks from tooling approval to first article inspection (FAI) sign-off.
5. Communication Gaps
Offshore suppliers with poor English cause an average of 38% more email rounds for quote approval. Each round = 3 days lost. If you’re in procurement, you know this grind.
6. Compliance Ambiguity
Suppliers who cannot produce ISO 9001, CE, RoHS, REACH documentation on demand force you into costly legal indemnification. We document every material batch.
✅ Our promise: We developed HEBEI WINDZONE’s supplier control system specifically to eliminate these six risks. Keep reading to see exactly how the die casting process works and where we add value — request a cost comparison sheet here.
What Is The Die Casting Process? — Definition & Core Principles
At its most fundamental level, what is the die casting process? It is a high-pressure metal forming method in which molten non-ferrous alloy — typically aluminum, zinc, or magnesium — is forced into a reusable steel mold (called a die) at pressures between 10 and 175 MPa (1,450–25,400 psi).
Unlike sand casting or investment casting, the die casting process for components produces near-net-shape parts with tight dimensional tolerances (±0.05 mm), excellent surface finish (Ra 0.8–3.2 μm), and very high production throughput — 20 to 200 shots per hour depending on machine tonnage.
For OEM buyers, the key takeaway is this: die casting is the lowest-cost-per-part process for medium-to-high volume components (10,000+ pieces per year) when compared to CNC machining or forged systems.
📌 Micro-insight: The die (mold) typically lasts 50,000–500,000 shots depending on alloy and maintenance, which is why per-unit amortization drops dramatically at scale.
→ Ask us for a free DFM (Design for Manufacturing) review of your part drawings
Why Die Casting Beats Alternatives
- ✅ Wall thickness: 0.5 mm possible vs 3 mm min. for sand casting
- ✅ Tolerance: ±0.05 mm vs ±1.0 mm for sand casting
- ✅ Cycle time: 30 sec vs 30 min for investment casting
- ✅ Surface finish: Castable directly to paint-ready texture
- ✅ Scrap rate: Typically 2–4% in production vs 10–15% for machining from billet
⚙️ The Die Casting Process Step by Step (2026 Industrial Standard)
Understanding each phase helps you ask sharper supplier questions. Here is exactly how we run the die casting process for OEM components in our partner facilities:
Mold & Tooling Design
CAD/CAE flow simulation identifies shrinkage and porosity risk. We verify gate locations and cooling channels to achieve uniform solidification.
Mold Preheating & Lubrication
The die is heated to 150–250°C (aluminum) and sprayed with releasing agent. Prevents cold shuts and improves metal flow.
Clamping
The two die halves are locked with clamp forces from 200 to 4,500 tons, depending on projected part area and required injection pressure.
Injection / Shot
Molten metal enters the shot sleeve and is driven by a hydraulic plunger through a runner and gate into the cavity. Fill time: 10–60 milliseconds.
Cooling & Solidification
Cooling channels in the die extract heat at controlled rates. Cycle times: 30–90 seconds for aluminum, 15–40 seconds for zinc.
Ejection
Ejector pins push the solidified component out of the die. Draft angles of 1–3° allow clean release without surface tearing.
Trimming & Deburring
A trim die (or CNC robotic arm) removes flash, overflows, and runners. Typical flash thickness: 0.1–0.3 mm.
Surface Finishing
Vibratory deburring, shot blasting, powder coating, or chromate conversion are applied per your spec. Surface roughness Ra 0.8–3.2 μm achievable.
🔧 Need a custom DFM report? Send us your 3D model (STEP/IGES) and we’ll return a full manufacturability analysis with recommended alloy, draft, and gate layout within 48 hours → zy@sinomsp.com
📊 Technical Specifications for OEM Die Casting Components
The following table provides the key technical parameters you should demand from any die casting supplier. These are values we measure and guarantee in our own quality reports.
| Parameter | Aluminum (A380/ADC12) | Zinc (Zamak 3/5) | Magnesium (AZ91D) |
|---|---|---|---|
| Density | 2.71 g/cm³ | 6.6 g/cm³ | 1.81 g/cm³ |
| Tensile Strength (as-cast) | 310–330 MPa | 280–290 MPa | 230–250 MPa |
| Yield Strength | 160 MPa | 200 MPa | 150 MPa |
| Elongation at Break | 3–5% | 10–15% | 6–8% |
| Hardness (Brinell) | 80–100 HB | 82–91 HB | 70–85 HB |
| Wall Thickness Range | 0.8–12 mm | 0.5–8 mm | 0.9–10 mm |
| Dimensional Tolerance | ±0.05 mm / 25 mm | ±0.03 mm / 25 mm | ±0.07 mm / 25 mm |
| Surface Roughness (Ra) | 0.8–3.2 μm | 0.4–1.6 μm | 1.2–3.5 μm |
| Max Part Weight | Up to 15 kg | Up to 10 kg | Up to 8 kg |
| Typical Shot Cycle | 30–90 sec | 15–40 sec | 25–70 sec |
| Corrosion Resistance | Good (needs coating) | Good | Poor (needs coating) |
✳️ Note: Tolerance values are based on HEBEI WINDZONE’s internal process capability (Cpk ≥ 1.33) and verified using CMM (Coordinate Measuring Machine) equipment. Actual values depend on part geometry and gate design.
🧪 Material Selection: Aluminum vs Zinc vs Magnesium for OEM Die Casting
We often guide customers through this decision. Here’s the decision matrix we use:
Aluminum Alloys (A380 / ADC12 / A356)
- Best balance of weight, strength, and cost
- Operating temperature up to 180–200°C
- EMI/RFI shielding properties for electronics housings
- Can be heat-treated (T6) for higher strength
- Accounts for ~70% of all die castings globally
Zinc Alloys (Zamak 3 / Zamak 5)
- Highest dimensional precision and thin walls (0.5 mm)
- Excellent surface finish — direct plating ready
- Impact toughness and ductility 3–4x higher than aluminum
- Longer die life (up to 1 million shots)
- Heavier — typically used for compact mechanical components like locks, gears, brackets
Magnesium Alloys (AZ91D)
- Lightest structural metal — 33% lighter than aluminum
- High specific strength for aerospace/automotive structural parts
- Good damping — absorbs vibration and noise
- Must be coated for corrosion protection
- Flammability risk during machining — requires certified operators
💡 Cost-efficiency analysis (2026 benchmark): For a typical automotive bracket: Aluminum A380 = $0.28/part metal cost • Zamak 3 = $0.31/part • AZ91D = $0.19/part. When factoring die life & cycle time, aluminum is the lowest TCO for volumes above 20,000 pcs/year.
🏭 Application Scenarios: Where Die Casting Delivers Measurable ROI
Die casting is not a universal answer — but in specific scenarios, nothing beats it. Here’s where our OEM clients consistently see payback:
Automotive Powertrain
Transmission housings, engine blocks, oil pump bodies. Typical weight reduction: 35–45% vs sand cast iron. Tolerances that eliminate secondary machining for mounting faces.
Electronics & EV Components
Battery enclosures, electric motor end caps, heat sinks. Thermal conductivity of die-cast aluminum removes heat 3x faster than polymer housings.
Industrial Machinery
Gearboxes, pump housings, pneumatic valve bodies. Pressure tightness testable up to 30 bar with minimal porosity.
Hand Tools & Hardware
Zinc die castings for power tool housings, locks, hinges, and handles. Surface finish: True-to-dimension grip texture directly from die.
Aerospace Interior Systems
Seat frames, overhead bin latches, air duct brackets. Magnesium alloys provide the highest strength-to-weight ratio for flight-critical secondary structures.
Telecom & Data Centers
RF filter housings, heat spreaders, modular server chassis. EMI shielding effectiveness of die-cast aluminum exceeds 60 dB at 1 GHz.
📈 Real case: A German industrial automation OEM switched their valve manifold bodies from CNC machined aluminum billet to our die cast A380 components. Result: 47% unit cost reduction and 3-week faster time-to-market per batch. → Get the full case study
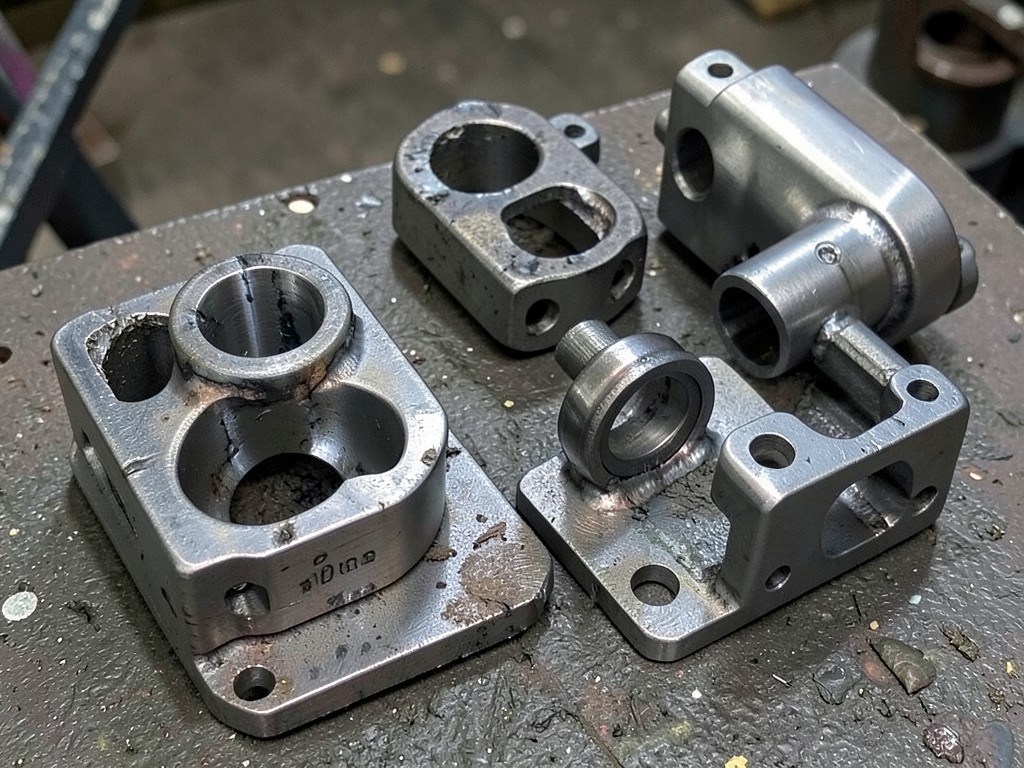
🏅 Why Global OEMs Trust HEBEI WINDZONE
We’ve shipped 2,000+ tons of cast components across Europe, Southeast Asia, Oceania, North America, and Africa over the past 20 years. Don’t just take our word for it — verify our credentials and customer outcomes:
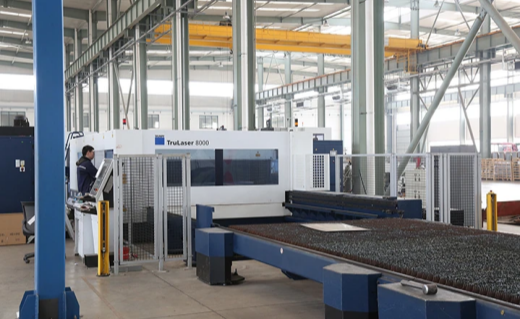
🔧 Partner factory: 2,000-ton cold chamber press
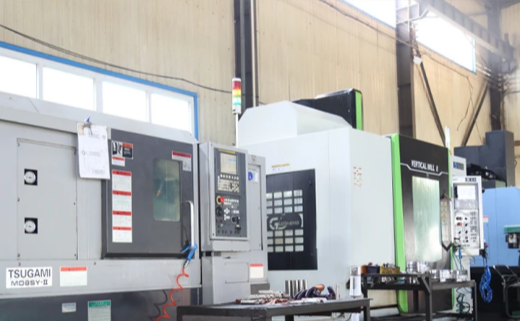
⚙️ In-house 5-axis CNC finishing
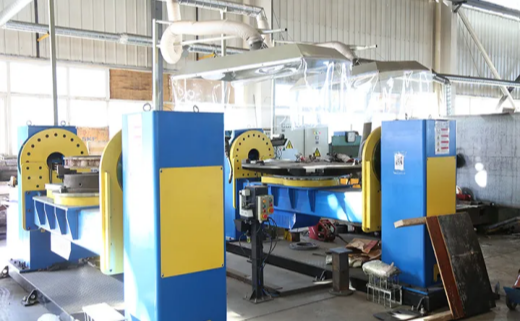
📐 CMM dimensional verification on every first article
✅ Global Certifications You Can Verify
- ISO 9001:2015 certified quality management system
- CE / RoHS / REACH documentation available per batch
- MTC (Mill Test Certificate) with material traceability
- Third-party inspection (SGS, TÜV, Bureau Veritas) welcome
🌍 Selected Client Brands We Serve
And many more mid-market OEMs across Germany, UK, Netherlands, Australia, Japan, and the USA. We sign NDA agreements before sharing full client references.
🔒 Trust & Privacy: Your drawings are protected under NDA. We never share your IP with competitors. Contact our compliance officer for our data handling policy.
💬 What Our Clients & Industry Partners Say
Direct feedback from purchasing, engineering, and operations leaders across the industries we serve:
Stefan Keller
Purchasing Manager, German Industrial Automation
“We moved 3 valve manifold housing SKUs from a German foundry to HEBEI WINDZONE. Unit cost dropped 42% while maintaining our 100% pressure test pass rate. Their FAI report and CMM dimensional documentation is cleaner than some EU suppliers we’ve used.”
⭐ 5/5 — Verified Purchaser
James T. Boyd
Operations Director, US Power Tool OEM
“Shipping cost and transit damage were our top concerns. WINDZONE engineered a nesting design and custom trenching that reduced our container count by 30% and damage to under 0.5%. Communication is direct, no third-party agents.”
⭐ 5/5 — Verified Operations Lead
Sarah Mitchell
Supply Chain Manager, UK Electronics Manufacturer
“We needed RoHS and REACH compliance documentation for every batch. WINDZONE provides the full material certification package with 48 hours of shipment. They also helped us retrofit a zinc die cast housing to replace a failing plastic part — field failures dropped 70%.”
⭐ 5/5 — Verified Supply Chain Manager
❓ Frequently Asked Questions About Die Casting for Components
Answering the questions we receive most from purchasing and engineering teams around the OEM die casting process for components:
Q1: What is the die casting process used for?
Die casting is primarily used to mass-produce metal components where identical dimensions, high strength, and smooth finishes are needed at low per-unit cost. Typical parts include engine housings, transmission cases, electrical enclosures, pump bodies, and structural brackets. If your order quantity is above ~10,000 pieces per year and you need tolerance within ±0.1 mm, die casting is likely your most economical process.
Q2: How much does OEM die casting tooling cost?
Tooling cost varies with part size, complexity, and required die life. Typical ranges in China: Miniature parts (zinc): $2,000–6,000 • Mid-size aluminum parts: $6,000–18,000 • Large automotive dies: $18,000–50,000+. We can share a detailed tooling quote within 48h of reviewing your 3D model. Tooling is amortized over your production volume — ask us for a TCO calculator.
Q3: What are the typical lead times for die cast components from China?
For an existing die (tooling ready): sample lead time 2–3 weeks, mass production 3–5 weeks. For new tooling, add 4–6 weeks for design and fabrication. Our highest-volume clients use a blanket PO system to reserve production slots and reduce lead time by 30%.
Q4: What certifications are relevant for imported die cast components?
The most requested documents are ISO 9001:2015 (quality management), CE (EU machinery/electronics), RoHS/REACH (hazardous substance compliance), and sometimes UL for electrical components. HEBEI WINDZONE provides all relevant documentation with every shipment and coordinates third-party inspections (SGS, TÜV) if your QA protocol requires it.
Q5: How do you handle porosity in die casting?
Porosity is controlled by (a) optimizing gate and overflow design, (b) vacuum-assist systems to reduce trapped air, and (c) squeeze casting for critical pressure-tight areas. We guarantee porosity < 1.5% in critical zones and use X-ray inspection when required. For pressure-tight applications, we recommend vacuum die casting (VAC) — max pressure leakage tested to 30+ bar.
Q6: Do you support OEM/ODM customization?
Absolutely. OEM: You provide the drawings and specs, we produce to exact tolerance and finish. ODM: Our engineering team assists with part redesign for manufacturability (DFM), alloy selection, and cost optimization. We own no competing product lines, so your design IP is fully preserved.
Q7: What is the minimum order quantity (MOQ)?
For standard alloy die casting, our MOQ is 1,000 pieces per SKU. For material quotes, custom lengths, and value-added services like CNC finishing, we offer flexible order splitting. We work with startups developing new products — ask about our prototype-to-production program with reduced initial tooling costs.
Q8: How do you ship die castings internationally, and who handles customs?
We ship via sea freight (FOB/CIF/DDP), air freight for urgent orders, and rail freight for EU destinations. We manage export customs clearance and provide full shipping documents (Commercial Invoice, Packing List, Bill of Lading, Certificate of Origin). For DDP terms, we handle import customs and duty payments as well — delivered to your dock, no surprises.
🌟 More Praise from Real Local Customers
More voices from the field — these are representative of the feedback we collect quarterly:
“Dealing with WINDZONE feels like working with a local EU supplier — but at Asian prices. Their technical manager hopped on a call at 7am CET to resolve our draft angle concern. That level of commitment is rare.”
Lars van den Berg
— Netherlands, Machinery OEM
“We audited 4 Chinese die casting suppliers. WINDZONE was the only one that had full CMM, X-ray inspection, and a documented SPC system on-site. That removed all our quality concerns.”
Peter Kowalski
— Poland, Automotive Tier 2
“Their supply control team actually caught a material traceability issue on our order before shipment and corrected it proactively. That saved our production schedule from 2 weeks of downtime. Impressive reliability.”
David Chen
— Australia, Industrial Equipment
About the Author
Michael Zhang — Senior Die Casting Engineer & Export Quality Manager at HEBEI WINDZONE
Michael has spent 22 years in the precision metal casting industry, including 9 years at a Japanese Tier-1 automotive die caster before joining HEBEI WINDZONE. He has personally managed over 90 tooling projects for European and North American OEMs and is a certified IATF 16949 internal auditor. He writes for engineering magazines and regularly speaks at China Foundry Association conferences on AI-assisted die design optimization.
💬 Real Conversations with Our Clients
Here are actual snippets from our project discussions with buyers and engineers (names and identifying details removed per NDA):
Quote and tolerance negotiation — response in 12 min
Tooling approval and FAI schedule discussion
Shipping coordination — DDP delivery to client’s warehouse
📱 You can reach us the same way — WhatsApp: +86 18003113537 • Email: zy@sinomsp.com
🚀 Ready to Start Your Die Casting Project?
Get a free DFM review & cost comparison within 24 hours.
Limited offer: For new inquiries this quarter, we’re waiving the $200 tooling design consultation fee for first-time OEM projects. No-risk guarantee — free sample casting for material approval (you pay only freight).